Metal Forgings Case Study: SA-182 F92 Alloy Steel Forged Rings Supplied to a European High-Pressure Valve OEM
Project Overview
In 2024, a European manufacturer of high-pressure ball valves and pipeline components approached Jiangyin Fangyuan Ringlike Forging And Flange Co., Ltd. (FY Forgings) with a demanding request: a reliable, audit-ready source of metal forgings for valve bodies, bonnets and seat rings used in supercritical steam and high-temperature hydrocarbon service. The customer had been buying from two regional forges, but chronic heat-treatment inconsistency and late deliveries were threatening their own assembly schedules.
| Project snapshot | Detail |
|---|---|
| Customer profile | European valve & pressure-vessel OEM (identity withheld by NDA) |
| Product scope | Metal forgings – alloy steel forged rings, valve body forgings, seat rings |
| Grades supplied | SA-182 F92, SA-182 F91, SA-182 F6NM (1.4313), F55 super duplex |
| Size range | OD up to 5,000 mm, single piece weight 10 kg – 10,000 kg |
| Annual volume | Approx. 1,800 tonnes in the first contract year |
| Delivery model | Rough machined, UT/MT tested, sea-worthy export packing |
The Challenge
F92 and F91 creep-strength steels are unforgiving. Small deviations in melting chemistry, forging ratio or tempering cycles show up later as unacceptable hardness scatter, poor Charpy impact values or cracking during the customer's own welding operations. The OEM's previous suppliers struggled with three specific issues:
- Chemistry drift on critical elements such as Cr, Mo, V and N, causing re-testing and scrap.
- Inconsistent normalizing and tempering, producing hardness spreads of more than 40 HB across a single batch.
- Documentation gaps – missing PED 3.1 certificates, incomplete UT reports and heat-number traceability that failed third-party inspection.
The customer also required a supplier capable of handling both large ring forgings and smaller, higher-volume valve seat rings on the same quality system, without shifting between workshops.
Our Solution
FY Forgings proposed a single-source programme built around open-die forging, ring rolling and in-house heat treatment, backed by full third-party inspection.
- Material and process review. Our metallurgists reviewed the customer's drawings and mapped each part to an optimised forging ratio, upsetting sequence and grain-flow direction, improving mechanical properties in the critical bore and flange sections.
- Controlled melting and forging. Electric-arc furnace plus ladle refining and vacuum degassing, with forging on presses up to 5,000 tonnes and ring rolling for seamless, symmetrical rings.
- Heat treatment discipline. Computer-controlled normalizing, quenching and tempering with chart-recorded cycles attached to every heat number; hardness verified at multiple positions per forging.
- Testing and certification. UT and MT to ASME / ASTM requirements, tensile and Charpy testing, PMI on 100% of finished parts, and PED 3.1 certificates together with ABS, BV, DNV, RINA, LR, NK, KR and CCS approvals where applicable.
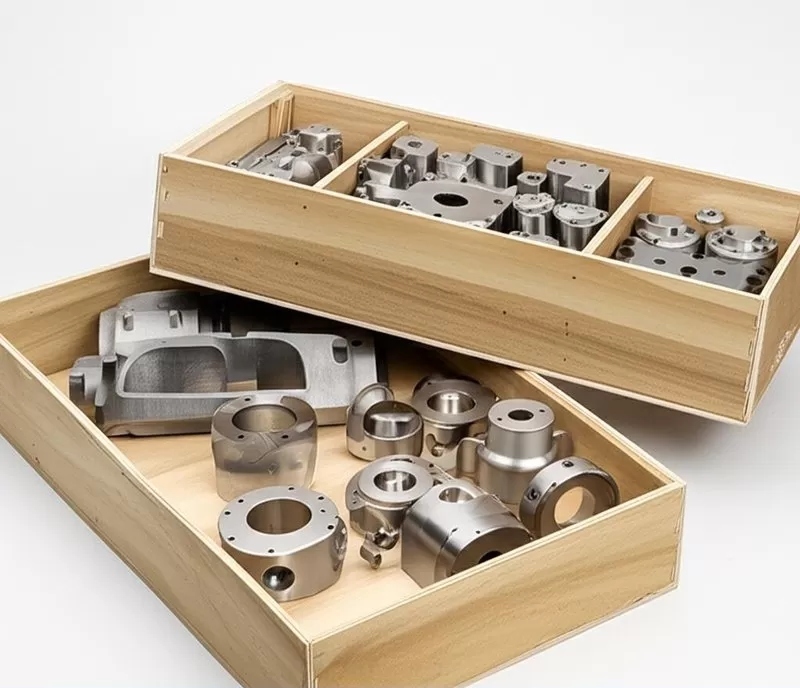
- Machining and packing. Rough or finish machining to drawing, with sea-worthy wooden cases and iron pallets designed for multimodal transport.
Results
| KPI | Before | After switching to FY Forgings |
|---|---|---|
| Incoming inspection rejection rate | 6.4% | 0.8% |
| Hardness spread within a batch | up to 45 HB | under 15 HB |
| Average lead time | 70–85 days | 30–45 days |
| Documentation non-conformities | 11 per year | zero in 18 months |
| Share of spend consolidated | — | two suppliers replaced by one |
Within three quarters the OEM had moved its entire F91/F92 valve forging package to FY Forgings, and later added F55 super duplex seat rings and F6NM gate components. Because the same plant handles melting, forging, heat treatment and machining, batch changes no longer trigger re-qualification delays.
Why It Worked
- 30+ years of forging experience – established in 1993, with 506 employees and an annual output capacity measured in tens of thousands of tonnes.
- Vertical integration – one quality system from steel to finished, rough-machined forging.
- Export-ready compliance – PED 3.1 and major classification-society approvals, familiar to European buyers and notified bodies.
- Engineer-to-engineer communication – technical queries answered with drawings and metallurgical data, not sales scripts.
Looking for a Metal Forgings Partner?
If you are qualifying a new source for alloy steel forgings, ring forgings, valve bodies or flanges in carbon steel, alloy steel, stainless steel or duplex grades, send us your drawings and specification. We will respond with a manufacturability review, proposed process route, indicative lead time and a sample qualification plan.

