Forged Steel Rings Case Study: Seamless Rolled Rings up to 18,000 kg for a North American Gearbox Manufacturer
Project Background
A North American manufacturer of heavy industrial gearboxes and bearing housings needed to replace a domestic ring-rolling supplier whose lead times had stretched beyond five months. The parts in question were forged steel rings used as gear blanks, bearing races and housing collars in mining conveyors and wind-turbine drive trains — large, thick-section rings where grain flow continuity and dimensional stability directly determine service life.
| Project snapshot | Detail |
|---|---|
| Customer profile | Heavy gearbox and bearing-housing OEM, North America (name withheld by NDA) |
| Product scope | Seamless rolled forged steel rings, ring blanks, collar rings |
| Material range | Carbon steel, alloy steel (42CrMo4 / 4140 class), stainless and duplex grades |
| Size capability used | Weight 50 kg – 18,000 kg; ID 50 mm – 6,500 mm; thickness 30 mm – 1,500 mm |
| Standards | ASTM, DIN, JIS, BS, GB — customer drawings take precedence |
| Contract volume | Approx. 2,600 tonnes per year across 19 part numbers |
What Made This Project Difficult
Rolled rings are not simple discs. Each ring is pierced, upset, rolled and then sized, and every step changes the wall-thickness uniformity the customer will later machine against. The OEM's specifications demanded:
- Seamless, directional grain flow — no welded or cut-and-rolled alternatives, because tangential grain flow is what gives a ring its fatigue resistance under rotating load.
- Wall-thickness tolerance within ±3 mm on rings up to 4.2 m outer diameter, to protect machining allowances.
- Through-hardening on thick sections — up to 1,200 mm wall on the largest bearing-race rings, verified by hardness mapping at three depths.
- Full traceability from heat number to finished ring, with UT and dimensional reports per piece.
- Export packing that survives ocean freight and inland rail without ovalisation or surface damage.
How FY Forgings Delivered
- Ring-rolling process design. For each of the 19 part numbers we defined blank weight, piercing diameter, rolling curve and sizing allowance, with a simulation check on the two largest sizes to confirm the mill could reach final wall thickness without re-heating.
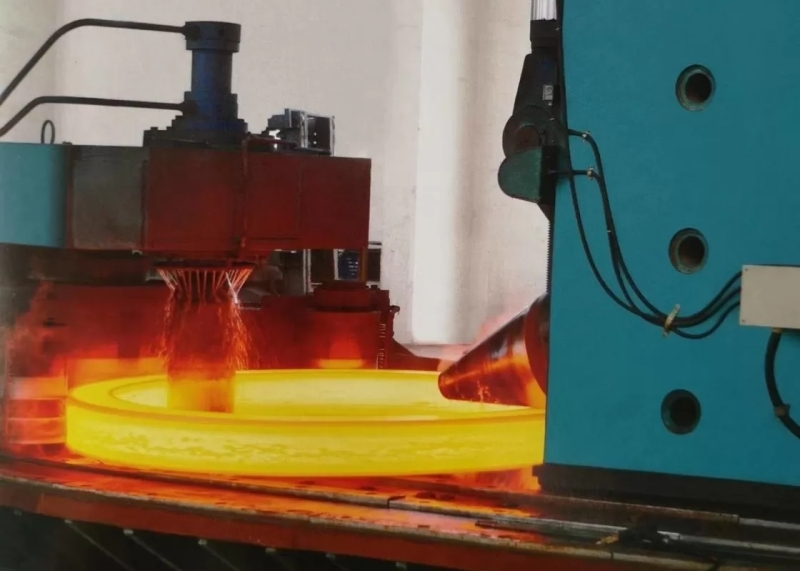
- Melting and forging. Electric-arc furnace with ladle refining and vacuum degassing, open-die upsetting on presses up to 5,000 tonnes, then radial-axial ring rolling for symmetrical, seamless rings.
- Heat treatment. Normalizing, quenching, tempering or solution annealing according to grade, with chart-recorded cycles and hardness verification per heat.
- Machining. Rough machining to drawing, with CNC vertical boring for large-diameter rings and dimensional reports issued per piece.
- Inspection and certification. UT and MT, PMI, dimensional and hardness reports, plus ISO, SGS, BV, ABS, GL-DNV, KR, LR and M650 certification as required.
- Packing. Sea-worthy wooden cases and pallets with radial bracing to prevent ovalisation during multimodal transport.
Results Achieved
| KPI | Previous supplier | After FY Forgings |
|---|---|---|
| Quoted lead time | 150–180 days | 45–60 days |
| Wall-thickness deviation | ±6 mm typical | ±3 mm or better |
| Machining allowance rework | 4 of 19 part numbers | zero after first article approval |
| Documentation completeness | partial | 100% per shipment |
| Transit damage claims | 3 in 12 months | zero in 14 months |
First-article rings for the two largest bearing races passed dimensional and metallurgical review without deviation, and the OEM consolidated all rolled-ring purchasing to FY Forgings within two quarters, later adding rough-machined rings to reduce internal turning load.
Why Buyers Choose Our Forged Steel Rings
- Genuine seamless rolled rings — no welded seams, continuous tangential grain flow.
- Wide size window — 50 kg to 18,000 kg, inner diameter up to 6,500 mm, thickness up to 1,500 mm.
- Material flexibility — carbon, alloy, stainless and duplex steels, to ASTM, DIN, JIS, BS and GB standards.
- In-house heat treatment and machining — one quality system from steel to finished ring.
- 30+ years of ring forging — established 1993, 506 employees, tens of thousands of tonnes annual capacity.
Send Us Your Ring Drawing
Tell us the outer diameter, inner diameter, thickness, weight, material grade and standard, and we will reply with a manufacturability review, proposed rolling route, heat-treatment cycle and indicative lead time — usually within two working days.

